CNC MACHINING CASE STUDY
Stainless Steel CNC Machining Optimized for an SS304 Cover Plate
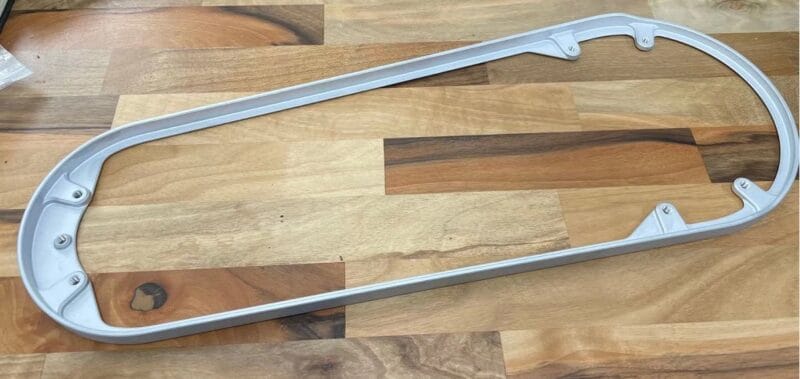
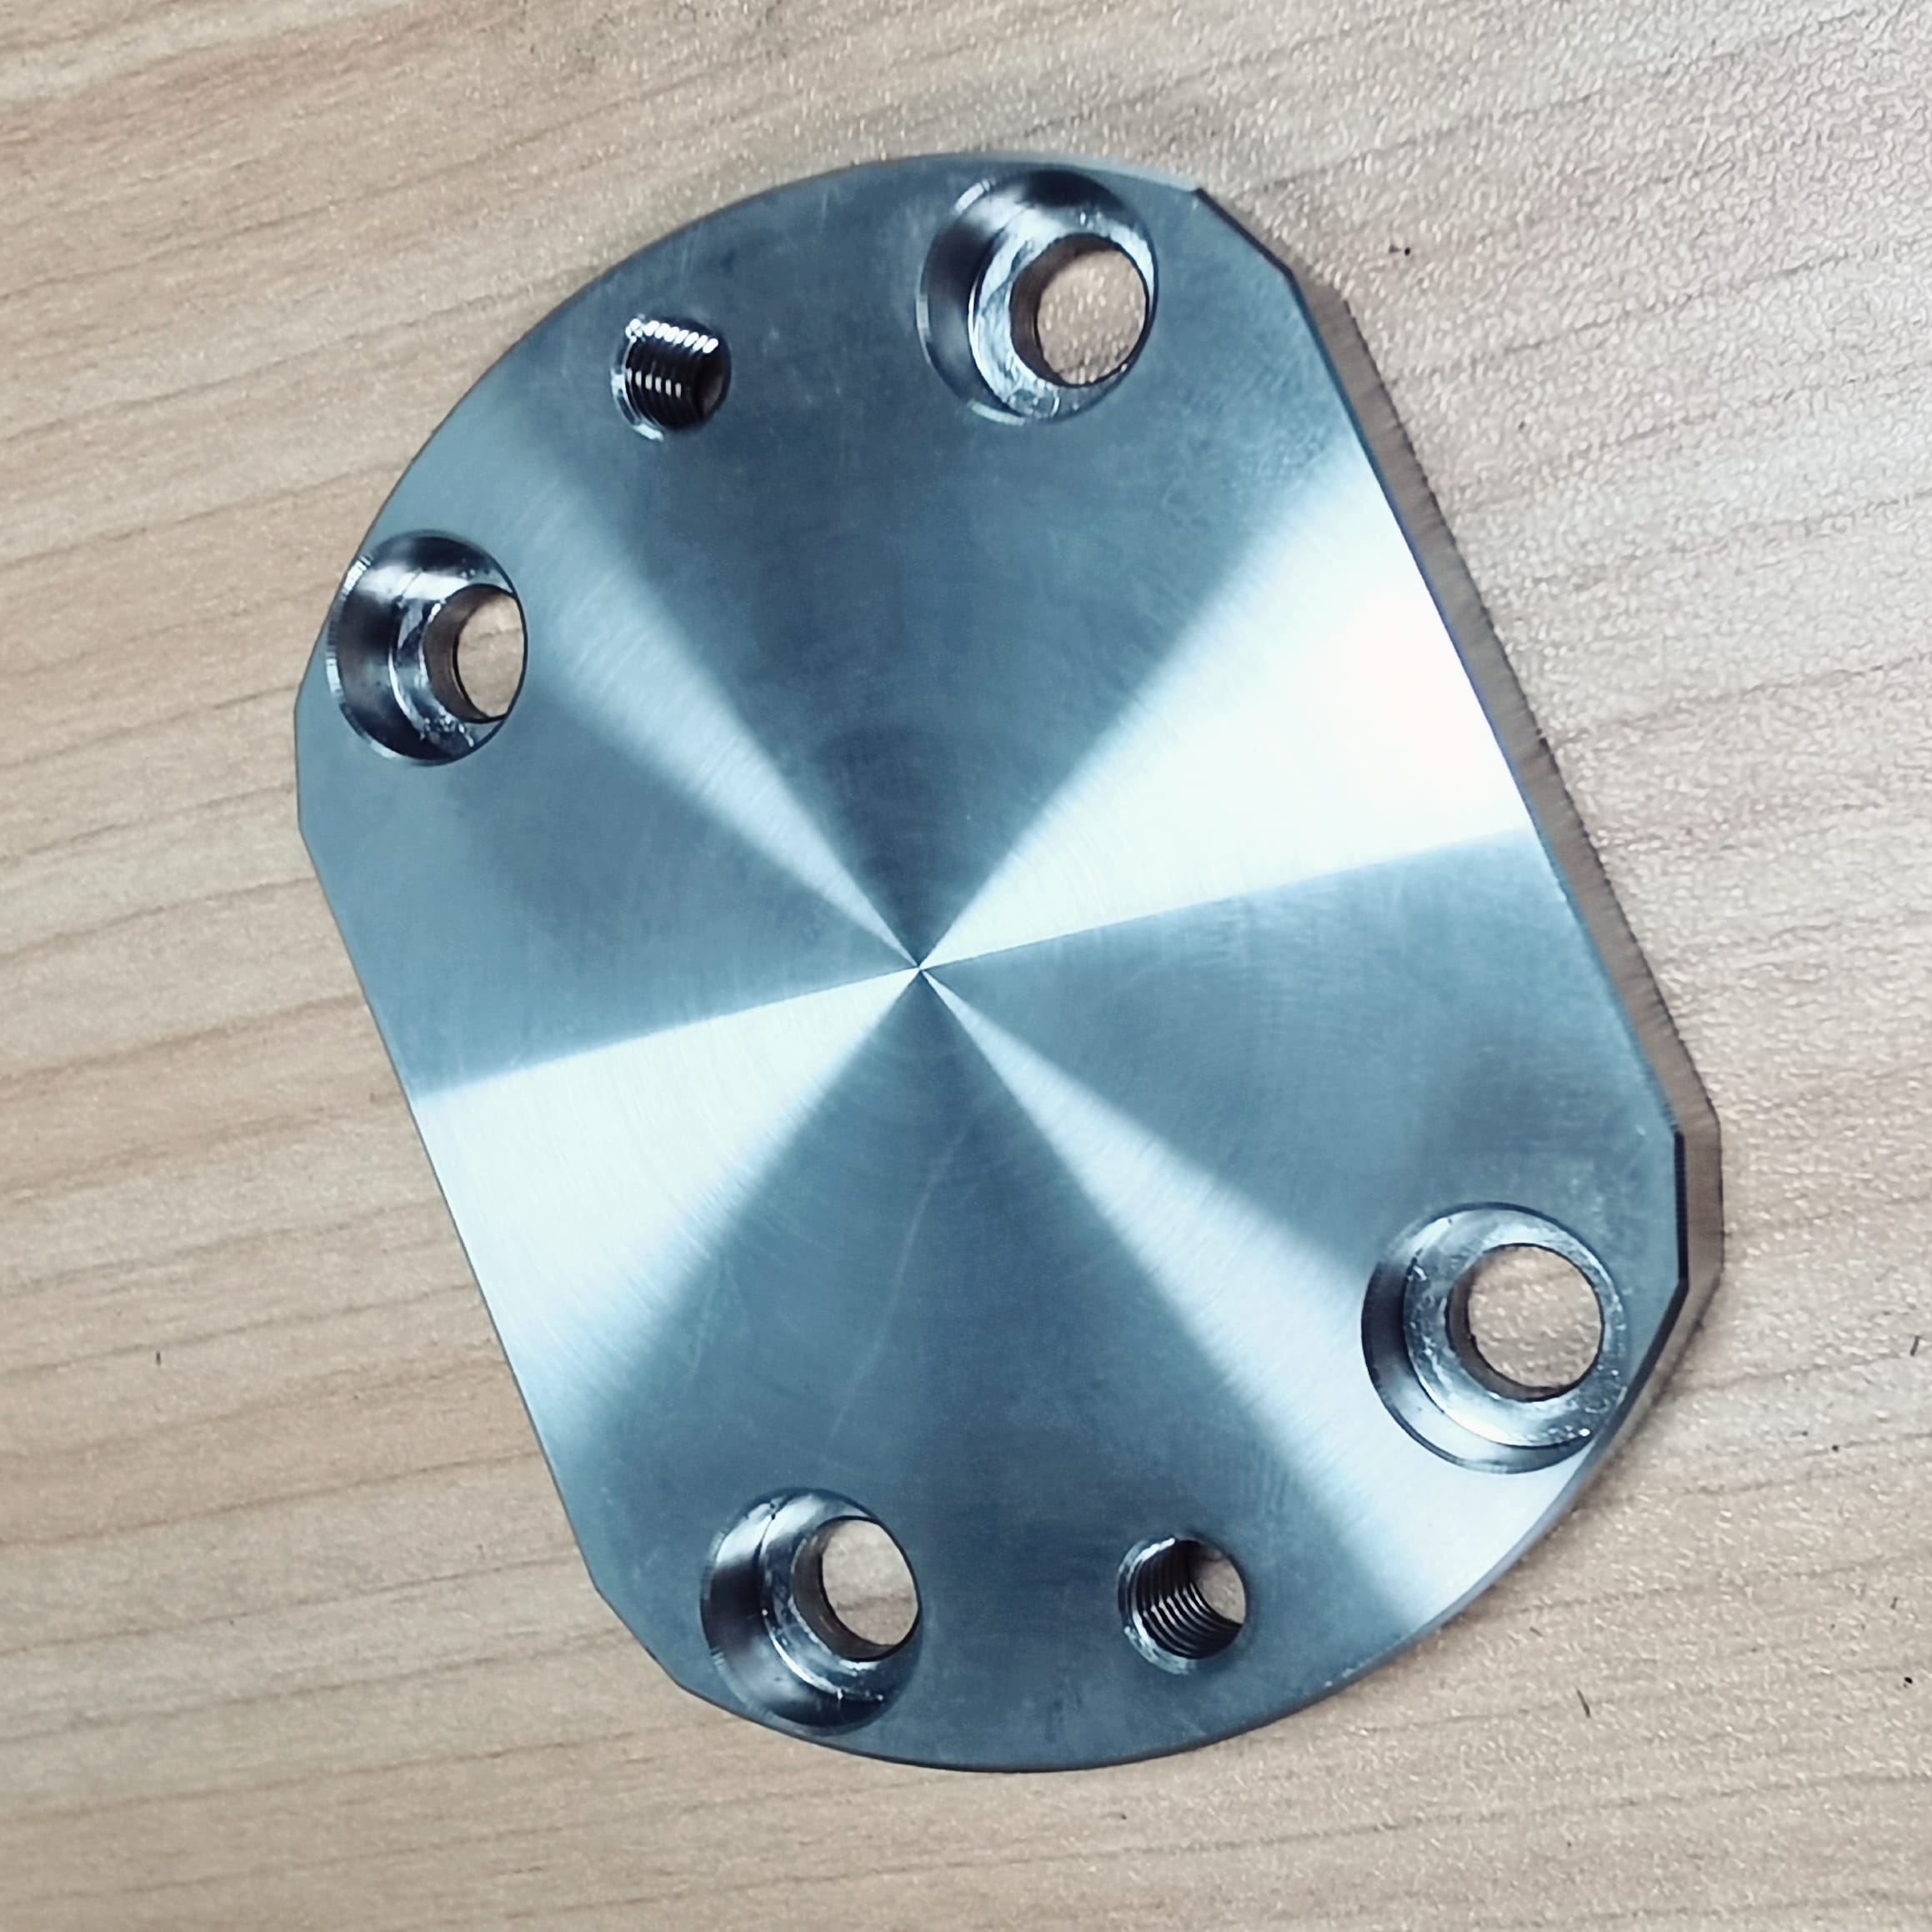
This case study shows how SPM improved stainless steel CNC machining for an SS304 cylinder cover plate by reviewing the complete production route instead of simply accepting an expensive finishing operation. The original process combined CNC turning and milling with double-side grinding to produce the required functional surface.
The challenge was that the SS304 part was non-magnetic, and the double-side grinding process operated at only about three pieces per hour. Grinding alone cost US$4.68 per part, making it the largest single process cost. By replacing this operation with finish turning while retaining the core CNC turning and milling operations, total manufacturing cost fell from US$6.55 to US$2.80 per part — a reduction of 57.3%.
Cylinder Cover Plate
SS304 Stainless Steel
500 pcs / month
Double-Side Surface Finishing
MANUFACTURING CHALLENGE
Why Double-Side Grinding Became the Main Cost Driver
At first glance, this component appears relatively straightforward. CNC turning and milling establish the primary geometry, followed by finishing of the two main surfaces. However, the economics of stainless steel CNC machining are not determined by geometric complexity alone. A seemingly simple finishing requirement can become the dominant cost when the selected process is slow or poorly matched to the material and production volume.
In the original production route, the non-magnetic SS304 component required double-side grinding after the main CNC operations. The grinding process ran at approximately three pieces per hour and added US$4.68 to every component. By comparison, CNC turning cost US$1.09 per part and CNC milling cost US$0.78.
This meant the finishing step cost considerably more than the two core machining processes combined. At a production volume of 500 pieces per month, repeating this low-efficiency operation in stainless steel CNC machining created a substantial recurring cost.
Original Process
Double-Side Grinding After CNC Machining
CNC turning: US$1.09 per part.
CNC milling: US$0.78 per part.
Double-side grinding: approximately 3 pcs/hour and US$4.68 per part.
Total: US$6.55 per part.
Optimized
Revised Process
Finish Turning Replaced Grinding
CNC turning: retained at US$1.09 per part.
CNC milling: retained at US$0.78 per part.
Finish turning: added at US$0.93 per part.
Total: reduced to US$2.80 per part.
PROCESS OPTIMIZATION
How Stainless Steel CNC Machining Replaced the Grinding Operation
The process review started by looking at the function of the grinding operation rather than treating grinding itself as a mandatory requirement. The engineering question was straightforward: was double-side grinding essential to the component, or was it simply the original method selected to create the required surface?
Once the finishing requirement was considered as part of the complete stainless steel CNC machining route, finish turning became a practical alternative. CNC turning and milling were already required to manufacture the part, so the revised route retained those operations and incorporated the final surface generation into machining instead of sending every component through a separate low-efficiency grinding process.
01
Compare the cost and purpose of turning, milling and double-side grinding rather than evaluating each operation independently.
02
Double-side grinding operated at only about three pieces per hour and accounted for US$4.68 of the original US$6.55 unit cost.
03
Finish turning was introduced to produce the required functional surface without the separate double-side grinding operation.
04
CNC turning and milling remained part of the production route and their original costs remained unchanged.
The result illustrates an important principle in stainless steel CNC machining: process optimization does not always require changing every operation. Sometimes the most effective improvement is to identify one disproportionately expensive step and determine whether its function can be achieved within another process that is already part of the manufacturing route.
SS304 PROCESS CONSIDERATIONS
Why the Complete Machining Route Matters for SS304 Parts
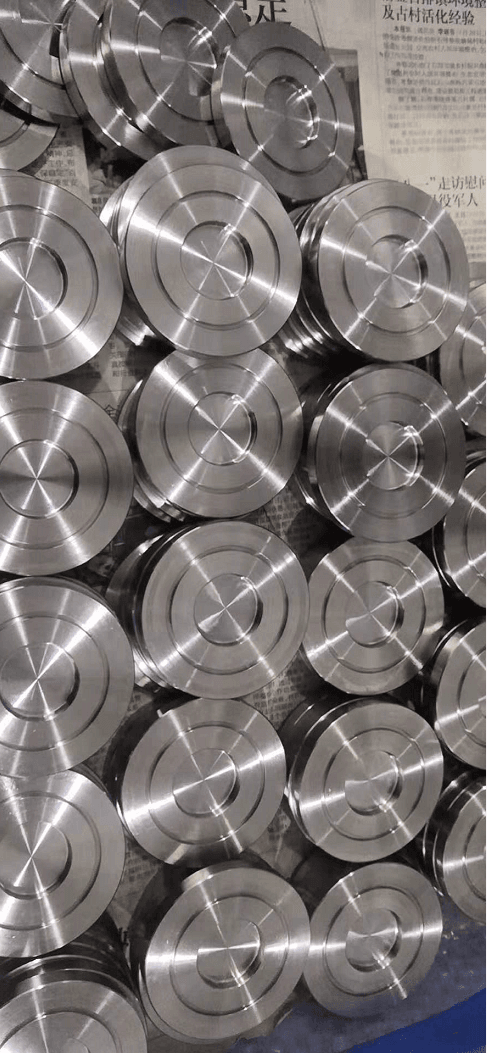
SS304 is an austenitic stainless steel widely used in manufactured components. When planning stainless steel CNC machining, the material specification is only one part of the production decision. The sequence used to generate the geometry and functional surfaces can have an equally important effect on cost, particularly when a separate secondary finishing operation is required.
Austenitic stainless steels also require appropriate machining practices. Technical guidance from the
Nickel Institute on machining austenitic chromium-nickel stainless steels
provides useful background on machining characteristics and practical considerations for this stainless-steel family.
In this project, the SS304 specification itself was not changed. The optimization instead focused on how the required part was manufactured. This distinction matters because cost reduction should not automatically mean substituting the specified material or compromising a functional requirement. A better stainless steel CNC machining strategy can sometimes be achieved by changing the process sequence while keeping the required material and core component function intact.
Review what each manufacturing operation must achieve before deciding how that operation should be performed. The required surface is the engineering objective; the original production method is not always the only route to achieve it.
COST BREAKDOWN
57.3% Cost Reduction Through Process Optimization
The financial effect of the revised stainless steel CNC machining route becomes significant at repeat-production volume. Eliminating US$4.68 of grinding cost and adding US$0.93 of finish turning produced a net saving of US$3.75 per component.
US$22,500
saved per year at 6,000 pcs / year
57.3% unit cost reduction
US$6.55 → US$2.80
US$3,275 → US$1,400
US$39,300 → US$16,800
| Process | Before (per pc) | After (per pc) | Change |
|---|---|---|---|
| CNC Turning | US$1.09 | US$1.09 | Unchanged |
| CNC Milling | US$0.78 | US$0.78 | Unchanged |
| Double-Side Grinding | US$4.68 | — | Eliminated |
| Finish Turning | — | US$0.93 | Added |
| Total per part | US$6.55 | US$2.80 | −57.3% |
| Total 500 pcs / month | US$3,275 | US$1,400 | −57.3% |
| Total 6,000 pcs / year | US$39,300 | US$16,800 | −57.3% |
CNC turning and milling did not become cheaper in the revised stainless steel CNC machining calculation; both remained exactly the same. The saving came from removing the US$4.68 double-side grinding operation and replacing it with US$0.93 of finish turning. This makes the source of the 57.3% reduction clear and avoids attributing the improvement to unrelated machining changes.
WHY THIS APPROACH WORKED
Optimize the Expensive Step, Not Every Step
Manufacturing cost reduction is sometimes approached by asking every supplier to reduce machining prices by a few percentage points. For this component, that strategy would have missed the main opportunity. Turning and milling together represented only US$1.87 of the original US$6.55 unit cost, while double-side grinding alone represented US$4.68.
The larger opportunity was therefore not to negotiate a small reduction in CNC turning or milling. It was to reconsider why the expensive grinding operation existed and whether the same functional objective could be reached differently. Once finish turning was introduced, the grinding operation could be removed from the stainless steel CNC machining process sequence.
Production quantity makes this type of review particularly relevant. A saving of US$3.75 may appear modest when looking at one component. At 500 parts per month, however, it becomes US$1,875 per month. Across 6,000 parts per year, the same process decision produces US$22,500 in annual savings.
Good Review Candidates
Look Closely at Secondary Operations
- A secondary process costs more than the core machining operations.
- Production throughput is limited by one slow finishing step.
- The same operation is repeated on hundreds or thousands of parts.
- The required function may be achievable through another existing process.
Keep the Engineering Requirement
Process Change Is Not Requirement Reduction
- Material requirements must still be respected.
- Critical part geometry still has to be produced.
- The required functional surface remains the objective.
- The revised process must make manufacturing sense at the target volume.
DFM FOR REPEAT PRODUCTION
Small Process Changes Can Create Large Annual Savings
This case also shows why DFM should not be limited to the shape of a component. For repeat-production stainless steel CNC machining, manufacturing sequence is part of design-for-manufacturing thinking. A drawing may be fully manufacturable and still leave room for a more efficient production route.
At prototype quantities, suppliers often prioritize flexibility because the cost of developing a specialized process may not be justified. At 500 components per month, the economics change. Every unnecessary minute and every avoidable secondary operation is repeated thousands of times over the life of the project.
That is why SPM evaluates the complete stainless steel CNC machining route when reviewing suitable repeat-production components. The goal is not to remove operations arbitrarily. It is to understand which processes create the required function, which processes create unnecessary recurring cost, and whether the two can be separated.
comparing only the price of individual CNC operations can hide the larger cost opportunity. For repeat orders, ask whether the complete manufacturing route has been reviewed before the process is locked for production.
WHY THIS MATTERS FOR YOUR RFQ
Review Stainless Steel CNC Machining Before Production Is Locked
For an RFQ involving stainless steel CNC machining, SPM looks beyond whether the drawing can simply be produced. Where appropriate, we also review the relationship between material, geometry, machining operations, finishing requirements and production quantity to identify avoidable recurring cost.
This SS304 cover plate is a straightforward example. The core turning and milling operations were not the problem. The cost bottleneck was a slow double-side grinding process added after machining. Replacing that operation with finish turning reduced total cost from US$6.55 to US$2.80 per part while preserving the required functional purpose described for the component.
The same 57.3% saving should not be expected for every project. The value of the example is the engineering approach: identify the actual cost driver first, then evaluate whether the production sequence can achieve the same required function more efficiently.
If you are sourcing a repeat-production stainless steel CNC machining project, you can also review our
other manufacturing case studies
to see how SPM approaches material utilization, machining strategy, tooling and process optimization across different components.
Have a Similar Part?
Send Your Drawing for a Manufacturing Review
Share your drawing, material, quantity and key requirements so our team can evaluate the manufacturing route.
CNC MACHINING CASE STUDY
Stainless Steel CNC Machining Optimized for an SS304 Cover Plate
This case study shows how SPM improved stainless steel CNC machining for an SS304 cylinder cover plate by reviewing the complete production route instead of simply accepting an expensive finishing operation. The original process combined CNC turning and milling with double-side grinding to produce the required functional surface.
The challenge was that the SS304 part was non-magnetic, and the double-side grinding process operated at only about three pieces per hour. Grinding alone cost US$4.68 per part, making it the largest single process cost. By replacing this operation with finish turning while retaining the core CNC turning and milling operations, total manufacturing cost fell from US$6.55 to US$2.80 per part — a reduction of 57.3%.
MANUFACTURING CHALLENGE
Why Double-Side Grinding Became the Main Cost Driver
At first glance, this component appears relatively straightforward. CNC turning and milling establish the primary geometry, followed by finishing of the two main surfaces. However, the economics of stainless steel CNC machining are not determined by geometric complexity alone. A seemingly simple finishing requirement can become the dominant cost when the selected process is slow or poorly matched to the material and production volume.
In the original production route, the non-magnetic SS304 component required double-side grinding after the main CNC operations. The grinding process ran at approximately three pieces per hour and added US$4.68 to every component. By comparison, CNC turning cost US$1.09 per part and CNC milling cost US$0.78.
This meant the finishing step cost considerably more than the two core machining processes combined. At a production volume of 500 pieces per month, repeating this low-efficiency operation in stainless steel CNC machining created a substantial recurring cost.
Double-Side Grinding After CNC Machining
CNC turning: US$1.09 per part.
CNC milling: US$0.78 per part.
Double-side grinding: approximately 3 pcs/hour and US$4.68 per part.
Total: US$6.55 per part.
Finish Turning Replaced Grinding
CNC turning: retained at US$1.09 per part.
CNC milling: retained at US$0.78 per part.
Finish turning: added at US$0.93 per part.
Total: reduced to US$2.80 per part.
PROCESS OPTIMIZATION
How Stainless Steel CNC Machining Replaced the Grinding Operation
The process review started by looking at the function of the grinding operation rather than treating grinding itself as a mandatory requirement. The engineering question was straightforward: was double-side grinding essential to the component, or was it simply the original method selected to create the required surface?
Once the finishing requirement was considered as part of the complete stainless steel CNC machining route, finish turning became a practical alternative. CNC turning and milling were already required to manufacture the part, so the revised route retained those operations and incorporated the final surface generation into machining instead of sending every component through a separate low-efficiency grinding process.
The result illustrates an important principle in stainless steel CNC machining: process optimization does not always require changing every operation. Sometimes the most effective improvement is to identify one disproportionately expensive step and determine whether its function can be achieved within another process that is already part of the manufacturing route.
SS304 PROCESS CONSIDERATIONS
Why the Complete Machining Route Matters for SS304 Parts
SS304 is an austenitic stainless steel widely used in manufactured components. When planning stainless steel CNC machining, the material specification is only one part of the production decision. The sequence used to generate the geometry and functional surfaces can have an equally important effect on cost, particularly when a separate secondary finishing operation is required.
Austenitic stainless steels also require appropriate machining practices. Technical guidance from the Nickel Institute on machining austenitic chromium-nickel stainless steels provides useful background on machining characteristics and practical considerations for this stainless-steel family.
In this project, the SS304 specification itself was not changed. The optimization instead focused on how the required part was manufactured. This distinction matters because cost reduction should not automatically mean substituting the specified material or compromising a functional requirement. A better stainless steel CNC machining strategy can sometimes be achieved by changing the process sequence while keeping the required material and core component function intact.
COST BREAKDOWN
57.3% Cost Reduction Through Process Optimization
The financial effect of the revised stainless steel CNC machining route becomes significant at repeat-production volume. Eliminating US$4.68 of grinding cost and adding US$0.93 of finish turning produced a net saving of US$3.75 per component.
57.3% unit cost reduction
| Process | Before (per pc) | After (per pc) | Change |
|---|---|---|---|
| CNC Turning | US$1.09 | US$1.09 | Unchanged |
| CNC Milling | US$0.78 | US$0.78 | Unchanged |
| Double-Side Grinding | US$4.68 | — | Eliminated |
| Finish Turning | — | US$0.93 | Added |
| Total per part | US$6.55 | US$2.80 | −57.3% |
| Total 500 pcs / month | US$3,275 | US$1,400 | −57.3% |
| Total 6,000 pcs / year | US$39,300 | US$16,800 | −57.3% |
CNC turning and milling did not become cheaper in the revised stainless steel CNC machining calculation; both remained exactly the same. The saving came from removing the US$4.68 double-side grinding operation and replacing it with US$0.93 of finish turning. This makes the source of the 57.3% reduction clear and avoids attributing the improvement to unrelated machining changes.
WHY THIS APPROACH WORKED
Optimize the Expensive Step, Not Every Step
Manufacturing cost reduction is sometimes approached by asking every supplier to reduce machining prices by a few percentage points. For this component, that strategy would have missed the main opportunity. Turning and milling together represented only US$1.87 of the original US$6.55 unit cost, while double-side grinding alone represented US$4.68.
The larger opportunity was therefore not to negotiate a small reduction in CNC turning or milling. It was to reconsider why the expensive grinding operation existed and whether the same functional objective could be reached differently. Once finish turning was introduced, the grinding operation could be removed from the stainless steel CNC machining process sequence.
Production quantity makes this type of review particularly relevant. A saving of US$3.75 may appear modest when looking at one component. At 500 parts per month, however, it becomes US$1,875 per month. Across 6,000 parts per year, the same process decision produces US$22,500 in annual savings.
Look Closely at Secondary Operations
- A secondary process costs more than the core machining operations.
- Production throughput is limited by one slow finishing step.
- The same operation is repeated on hundreds or thousands of parts.
- The required function may be achievable through another existing process.
Process Change Is Not Requirement Reduction
- Material requirements must still be respected.
- Critical part geometry still has to be produced.
- The required functional surface remains the objective.
- The revised process must make manufacturing sense at the target volume.
DFM FOR REPEAT PRODUCTION
Small Process Changes Can Create Large Annual Savings
This case also shows why DFM should not be limited to the shape of a component. For repeat-production stainless steel CNC machining, manufacturing sequence is part of design-for-manufacturing thinking. A drawing may be fully manufacturable and still leave room for a more efficient production route.
At prototype quantities, suppliers often prioritize flexibility because the cost of developing a specialized process may not be justified. At 500 components per month, the economics change. Every unnecessary minute and every avoidable secondary operation is repeated thousands of times over the life of the project.
That is why SPM evaluates the complete stainless steel CNC machining route when reviewing suitable repeat-production components. The goal is not to remove operations arbitrarily. It is to understand which processes create the required function, which processes create unnecessary recurring cost, and whether the two can be separated.
WHY THIS MATTERS FOR YOUR RFQ
Review Stainless Steel CNC Machining Before Production Is Locked
For an RFQ involving stainless steel CNC machining, SPM looks beyond whether the drawing can simply be produced. Where appropriate, we also review the relationship between material, geometry, machining operations, finishing requirements and production quantity to identify avoidable recurring cost.
This SS304 cover plate is a straightforward example. The core turning and milling operations were not the problem. The cost bottleneck was a slow double-side grinding process added after machining. Replacing that operation with finish turning reduced total cost from US$6.55 to US$2.80 per part while preserving the required functional purpose described for the component.
The same 57.3% saving should not be expected for every project. The value of the example is the engineering approach: identify the actual cost driver first, then evaluate whether the production sequence can achieve the same required function more efficiently.
If you are sourcing a repeat-production stainless steel CNC machining project, you can also review our other manufacturing case studies to see how SPM approaches material utilization, machining strategy, tooling and process optimization across different components.
Send Your Drawing for a Manufacturing Review
Share your drawing, material, quantity and key requirements so our team can evaluate the manufacturing route.