CNC MACHINING CASE STUDY
Wire EDM Machining Optimized for an AISI 420 Helical Pin Guide
This case study shows how SPM reduced the manufacturing cost of an AISI 420 helical pin guide by reviewing the wire EDM machining strategy instead of treating the original process route as fixed. The initial design used mirror EDM for the critical Ra 0.4 surfaces, while CNC turning produced the Ra 1.6 surfaces.
Mirror EDM became the dominant cost driver at US$38.75 per part. By redesigning the process around angled slow wire cutting, CNC turning and milling, SPM retained the required Ra 0.4 surface while reducing total unit cost from US$41.62 to US$14.42. At 120 parts per month, the revised process reduced unit cost by 65.4% and generated annual savings of US$16,320.
DESIGN & PROCESS CHANGE
From Mirror EDM to an Optimized Wire EDM Machining Route
The important change was not a reduction in surface quality. SPM reconsidered how the critical surfaces should be produced and compared the original process with a more efficient wire EDM machining route. The Ra 0.4 requirement remained unchanged throughout the review.
MANUFACTURING CHALLENGE
Why Mirror EDM Became the Main Cost Bottleneck
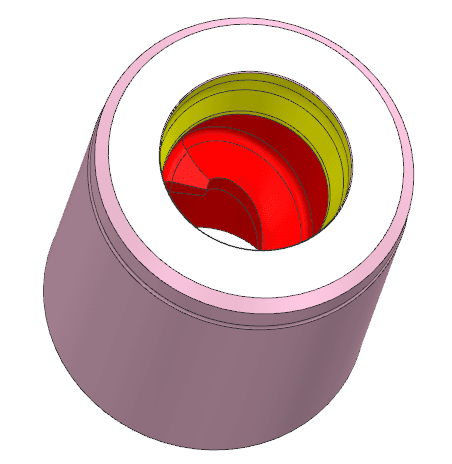
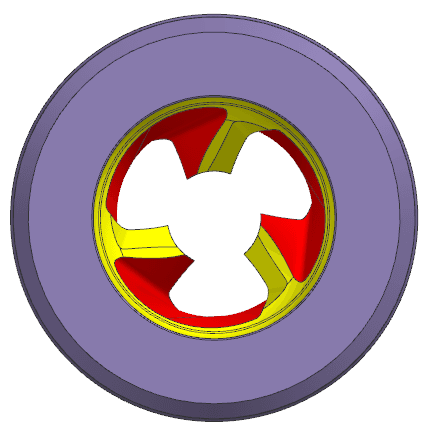
The component contained two different surface-finish requirements. The Ra 1.6 surfaces could be produced by CNC turning, but the critical Ra 0.4 surfaces were assigned to mirror EDM. Technically, the original process could manufacture the component. Commercially, however, it created a disproportionately high unit cost for repeat production.
The engineering question was therefore whether the Ra 0.4 requirement actually depended on mirror EDM, or whether another wire EDM machining strategy could achieve the required result while preserving the intended component performance.
Mirror EDM Dominated the Cost
Ra 0.4 surfaces: Mirror EDM at US$38.75 per part.
Ra 1.6 surfaces: CNC turning only.
Total cost: US$41.62 per part.
Angled Slow Wire Cut Replaced Mirror EDM
Ra 0.4 surfaces: Slow wire cut with angle.
Ra 1.6 surfaces: CNC turning plus milling.
Total cost: US$14.42 per part.
ENGINEERING DECISION
How Wire EDM Machining Changed the Process Economics
The optimization began by separating the engineering requirement from the manufacturing method originally selected to produce it. The drawing required Ra 0.4, but mirror EDM itself was not the functional requirement. This allowed SPM to evaluate a different wire EDM machining route without changing the critical surface target.
PRODUCTION RESULT
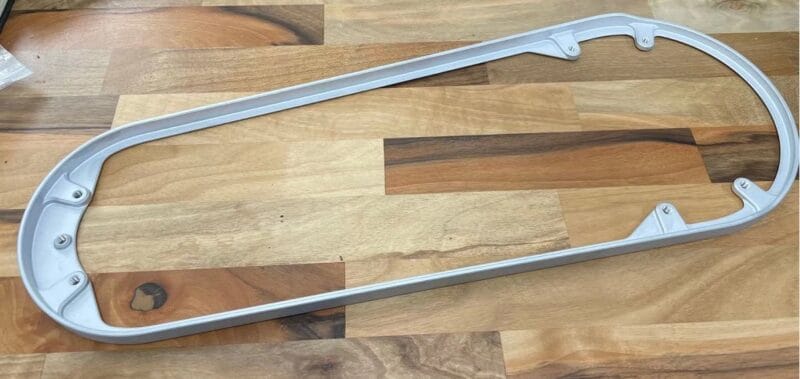
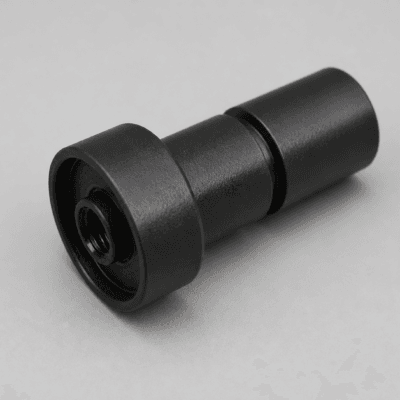
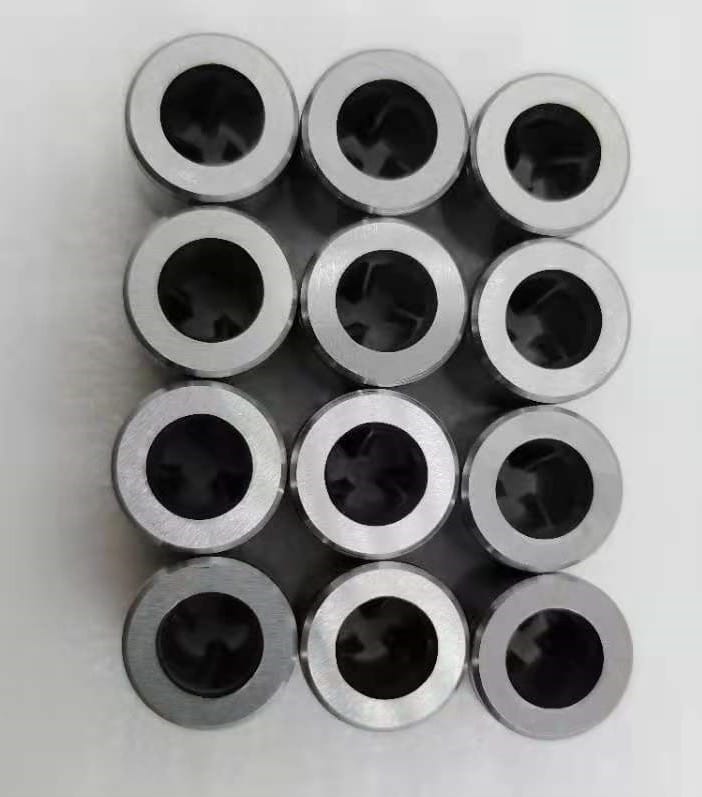
Finished AISI 420 Helical Pin Guides
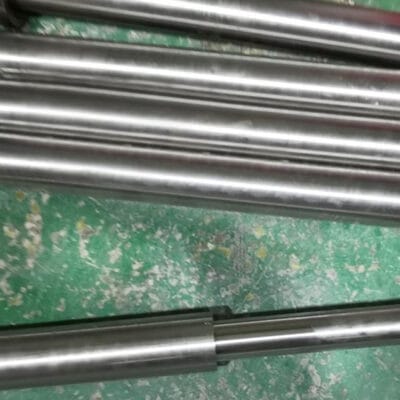
After the process redesign, production used the revised combination of angled slow wire cutting, CNC turning and milling. The finished parts below show the production result after the manufacturing route was optimized.
WIRE EDM & SURFACE FINISH
Surface Requirement First, Manufacturing Method Second
A surface-finish specification should be treated as an engineering result rather than an automatic instruction to use one particular manufacturing process. The objective is to determine which process route can achieve the required surface efficiently while remaining practical for repeat production.
In this project, the Ra 0.4 requirement remained unchanged while the production method was reconsidered. This distinction is especially relevant in wire EDM machining, where geometry, cutting strategy, angle and required surface quality influence how the process should be planned.
The cost reduction did not come from relaxing the specified finish. It came from changing how that finish was produced within the complete manufacturing route.
The component also required an angled cutting strategy. Instead of relying on mirror EDM for the critical surfaces, the revised wire EDM machining process used slow wire cutting with angle and redistributed the remaining operations to CNC turning and milling.
For additional technical background on electrical discharge machining and EDM equipment configurations, the Loughborough University EDM facility overview provides a useful non-commercial technical reference.
COST BREAKDOWN
65.4% Unit Cost Reduction Through Process Redesign
The financial benefit came from eliminating the US$38.75 mirror EDM operation and replacing it with a combination of wire EDM machining, CNC turning and milling. Although the revised route included several individual operations, their combined cost remained substantially lower than the original process.
65.4% unit cost reduction
| Process | Before | After | Change |
|---|---|---|---|
| Mirror EDM | US$38.75 | — | Eliminated |
| CNC Turning | US$2.87 | US$3.89 | Added scope |
| Slow Wire Cut with Angle | — | US$9.30 | Added |
| CNC Milling | — | US$1.23 | Added |
| Total per part | US$41.62 | US$14.42 | −65.4% |
| Total 120 pcs / month | US$2,081 | US$721 | −65.4% |
| Total 1,440 pcs / year | US$24,972 | US$8,652 | −65.4% |
CNC turning increased from US$2.87 to US$3.89, angled slow wire cutting added US$9.30, and CNC milling added US$1.23. Even with those additional operations, the revised wire EDM machining route cost only US$14.42 per component, a saving of US$27.20 compared with the original route.
ENGINEERING VALUE
Challenge the Cost Driver Instead of Negotiating Around It
A small percentage reduction in the price of mirror EDM would not have changed the economics of this component enough. The larger opportunity was to question whether the expensive operation itself was necessary to achieve the specified surface result.
Reviewing wire EDM machining together with turning and milling can therefore be more useful than treating EDM as an isolated specialty process. For some precision components, the better solution comes from redistributing the work across several operations rather than trying to make one expensive operation slightly cheaper.
When Process Redesign Is Worth Evaluating
One EDM operation represents a large share of total manufacturing cost.
The surface requirement must remain, but the original process itself is not fixed.
The component contains angled or difficult geometry.
Recurring volume allows unit savings to accumulate over time.
Cost Reduction Cannot Replace Part Requirements
Required surface finish still has to be maintained.
Geometry and material requirements remain controlled.
The revised process must remain practical for repeat production.
The complete process cost should be evaluated rather than one operation alone.
DFM FOR PRECISION PARTS
Why the Manufacturing Route Matters Before Production Is Locked
This project demonstrates why DFM should include process selection as well as component geometry. A part can be completely manufacturable and still be unnecessarily expensive because the initial production route is not the most economical option for recurring production.
For repeat-production wire EDM machining, process selection becomes more important as volume increases. In this case, the difference between the original and revised routes was US$27.20 per part. Monthly manufacturing cost fell from US$2,081 to US$721, while annual cost dropped from US$24,972 to US$8,652.
This type of review is most useful before a recurring production route becomes fixed. Comparing the full process sequence can reveal whether one specialized operation is creating a disproportionate share of total cost. A lower manufacturing cost does not always require a material change or a relaxed specification. Sometimes the greater opportunity comes from reviewing how the required geometry and surface condition are created across the complete process chain.
Quoting directly from a drawing is therefore only part of the job. A supplier that understands turning, milling and wire EDM machining as one integrated process stack may identify a more economical production route before an unnecessarily expensive method becomes established.
WHY THIS MATTERS FOR YOUR RFQ
Review Wire EDM Machining Before Finalizing the Process Route
For a precision component involving wire EDM machining, SPM reviews the relationship between geometry, surface requirements, material, machining sequence and production quantity. The objective is to identify expensive process assumptions before they become recurring production costs.
In this helical pin guide project, the Ra 0.4 requirement was preserved while the original mirror EDM route was removed. The final combination of angled slow wire cutting, CNC turning and milling reduced total unit cost from US$41.62 to US$14.42 without changing the critical surface requirement.
Not every wire EDM machining project will generate a 65.4% saving. The transferable lesson is the engineering method: identify the functional requirement, locate the dominant cost driver, evaluate alternative manufacturing routes and compare the complete production cost before the process becomes fixed.
You can also review our other manufacturing case studies to see how SPM approaches machining strategy, material utilization and process optimization across different components.
Send Your Drawing for a Manufacturing Review
Share your drawing, material, quantity and critical requirements so our team can evaluate the complete manufacturing route.